Operator handover succeeds when the receiving team can reproduce the approved process routine, recognize when conditions have changed, and respond within its authority. Watching an experienced commissioning engineer operate a feed pellet machine is not enough. The engineer may make small adjustments based on observations that were never explained, while the written instructions describe only the obvious controls. Buyers should therefore treat handover as a demonstration of transferable operating competence. The focus is a clear, repeatable method for starting, stopping, changing products, recording exceptions, and communicating unresolved issues without relying on undocumented habits or unsafe shortcuts.
Start From the Installed Process and Approved Instructions
Build the handover around the actual line, its controls, and the supplier’s approved instructions. Identify the machines that must be ready before the press can operate and the downstream conditions that permit material flow. Confirm that labels in the instructions match equipment labels and screen names. A generic procedure copied from another plant may describe similar machinery but different permissions, transfer arrangements, or utility responsibilities. Resolve these differences before assessing whether an operator can follow the routine independently.
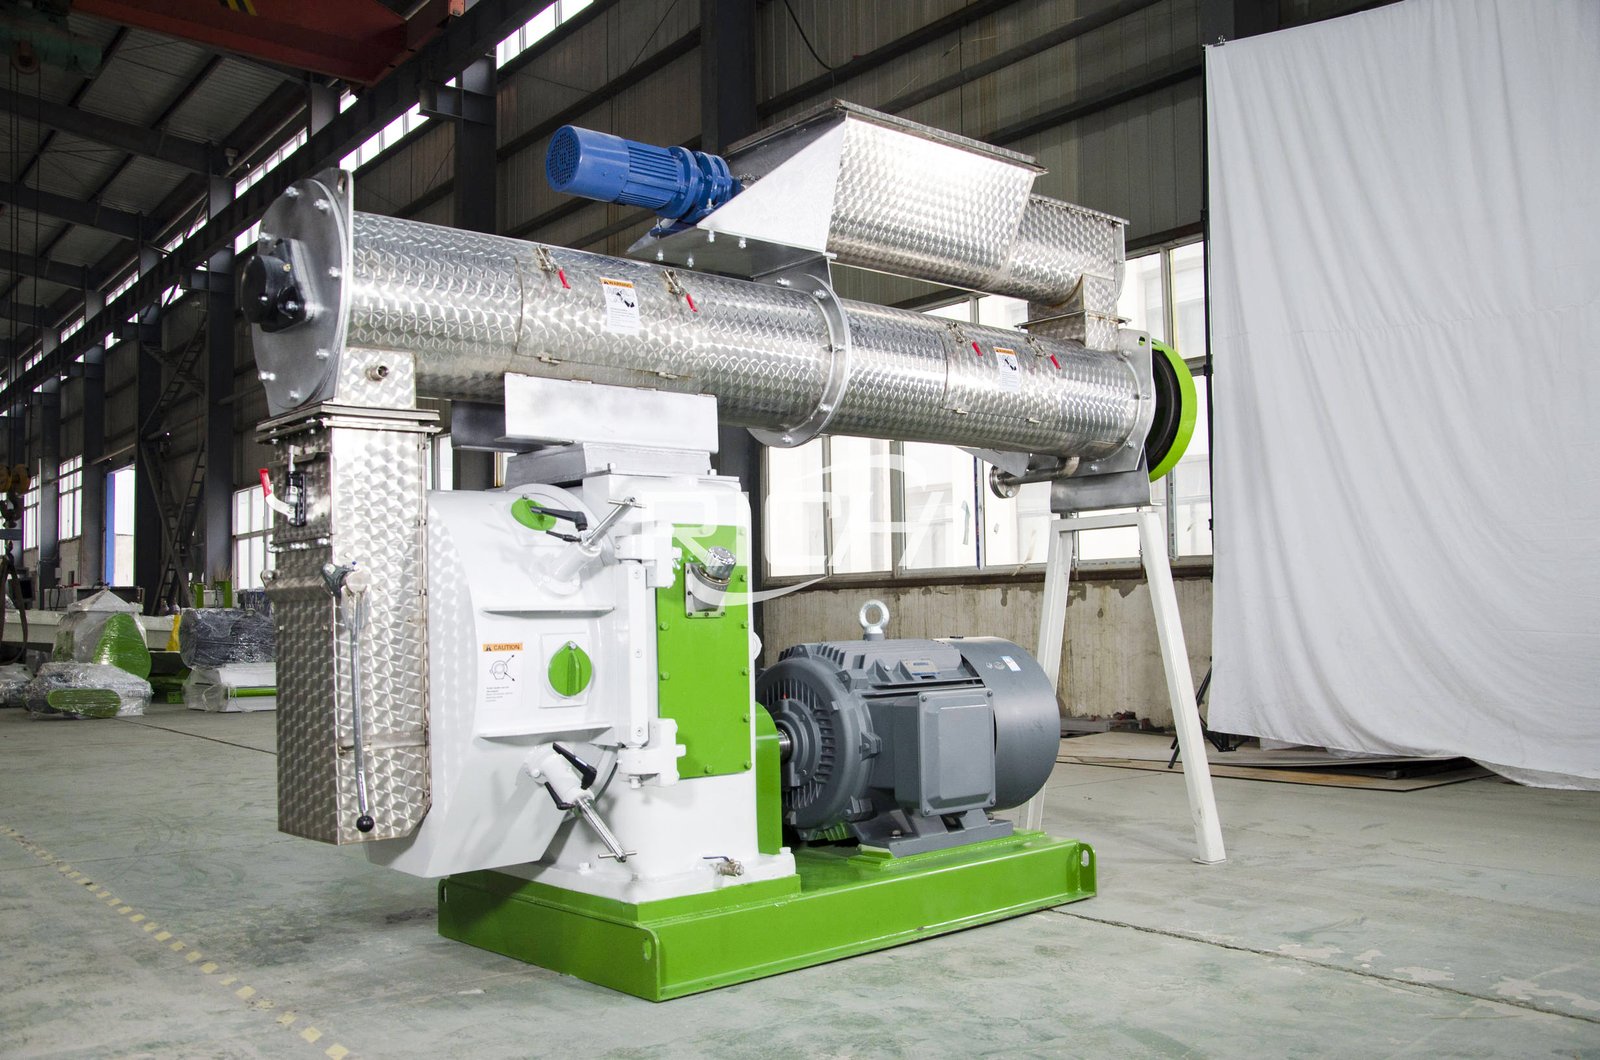
When the buyer reviews the feed pellet machine operating configuration with RICHI Machinery, use the installed equipment documentation to turn the commercial scope into a practical operating map. The handover should show where the operator’s responsibility begins and ends, and when maintenance, quality, utilities, or the supplier must be involved. Avoid defining competence as the ability to keep the machine running at any cost. A competent operator also knows when the approved routine no longer applies and when the correct response is to stop and escalate.
Teach the Reason Behind Each Readiness Check
Before startup, operators need a structured review of material identity, preparation status, equipment availability, utility conditions, product destination, and required records. Explain the purpose of each check so the team can recognize a relevant change rather than simply tick a box. For example, confirming the product destination prevents a successful startup from immediately creating a downstream bottleneck. Confirming the ingredient batch connects later quality observations with the material actually processed rather than with an expected formulation that was never supplied.
Keep checks appropriate to the operator’s role. Electrical, mechanical, and safety-related inspections that require specialist competence should remain with authorized personnel. Operators should receive a clear readiness indication and know what an incomplete indication means. They should not be asked to infer that a protective function is acceptable from the appearance of a screen. The handover record should show who performs each prerequisite check, what evidence is retained, and which unresolved conditions prohibit proceeding into the startup sequence.
Make Startup a Controlled Sequence Rather Than a Memory Test
Train the startup sequence using the equipment supplier’s procedure and the site’s approved operating method. Describe the expected state at each stage and the observation that confirms progression is permitted. Keep material introduction, utility coordination, and downstream readiness connected rather than teaching the press as an isolated machine. Operators should understand what normal early observations look like and which deviations require a pause. Specific settings and limits must come from the accepted configuration and equipment documentation, not from an unrelated commissioning example.
Use an operator-led demonstration after instruction. The trainer should observe and ask the operator to explain the next step without silently taking over every decision. Record where prompts were needed and whether the instruction lacked clarity. This is a learning exercise before it becomes a competence assessment. If the operator can perform the sequence only while the commissioning engineer points to controls, the knowledge has not yet been transferred. Revise the instruction or training plan and repeat the relevant demonstration under the agreed safe conditions.
Define What Operators May Adjust During Stable Running
Create an authority matrix for operating adjustments. Identify settings that the operator may change within approved limits, changes that require supervision, and changes reserved for specialist personnel. Explain how a change should be recorded and how the process response will be evaluated. Operators should not have to guess whether a quality problem authorizes a die-related intervention or a controls change. The approved operating window should provide context, while the authority matrix preserves the distinction between routine operation and troubleshooting work.
Teach observation before adjustment. The operator should check material identity, current process condition, quality observations, and recent events before attributing a problem to a single setting. When practical, change one authorized variable at a time and record the time and reason. Simultaneous unrecorded adjustments make later troubleshooting difficult and can conceal a utility or ingredient preparation problem. The handover should reinforce the habit of comparing current conditions with the documented baseline rather than copying a setting that happened to work during another product campaign.
Distinguish Planned Stops From Abnormal Stops
The receiving team needs separate, approved responses for planned shutdowns, short interruptions, and abnormal events. These conditions may require different handling of material, utilities, downstream equipment, and restart permission. Train the relevant procedures using the supplier’s instructions and site controls. A routine that is suitable for an ordinary end-of-shift stop should not automatically be applied after an alarm or a suspected mechanical problem. The operating record should identify the reason for the stop and the decision that permitted the next action.
After an abnormal stop, establish how the equipment state is communicated and who may authorize restart. Operators should preserve the event information and avoid repeatedly resetting an alarm without investigating it. Work requiring access to equipment must follow the site’s isolation and permit procedures and be performed by authorized people. Handover must never teach bypassing guards or protective functions as an effective production technique. The useful skill is recognizing the boundary of the operator’s authority and communicating enough information for the next responsible person to respond efficiently.
Treat Product Changeover as a Traceability Decision
A product changeover involves more than selecting another recipe or changing a label. Identify the outgoing and incoming formulations, the required preparation, material destinations, and quality controls. The approved changeover method should address carryover according to the plant’s product and quality requirements. Record how remaining material, transition product, and cleaning or flushing material are identified and handled. Do not assume that a previous production site’s method is suitable for every formulation or every quality assurance system.
Explain the release boundary between products. Quality staff should define how the incoming product becomes eligible for normal collection, storage, or sale. Operators should know which samples or checks are needed and what to do while waiting for release. The handover record should connect the product transition with the equipment condition and relevant settings. If a changeover requires a different approved component arrangement or specialist intervention, show the responsibility and verification steps clearly. Product identity must remain understandable even when the transition is interrupted or continues across shifts.
Build a Shift Log That Supports the Next Operator
A useful log records product identity, ingredient batch, approved settings, interruptions, quality observations, outstanding actions, and the current equipment state. Keep routine entries concise enough to complete reliably. More detailed event records should capture the time, observation, action, and response when the process deviates from its baseline. A log filled with normal-operation marks but no explanation of significant changes cannot support an effective handover. The next operator needs to understand what happened, what remains unresolved, and which instructions currently apply.
Include an explicit shift-to-shift exchange rather than relying only on a completed form. The outgoing operator should explain pending product decisions, recurring observations, or temporary constraints within the approved operating method. The incoming operator should confirm the current status before taking responsibility. Supervisors should review whether the written record and verbal exchange agree. This prevents an unresolved commissioning action from becoming an accepted habit simply because it has been repeated for several shifts without anybody recognizing it as an exception.
Assess Competence Using Scenarios and Evidence
Assessment should cover ordinary startup, stable running, planned stop, a representative changeover, and communication of an abnormal condition. Use safe demonstrations and discussion where creating a real fault would be inappropriate. Ask operators to explain the evidence they would check, the action permitted by the procedure, and when they would escalate. Record the outcome by task rather than issuing a broad competence statement based on attendance. Understanding one part of the line does not establish readiness for every product or operating condition.
Identify remaining support needs honestly. A new operator may be ready for a defined product routine while still requiring supervision for a more complex changeover. State that limitation and plan the additional instruction. Where several shifts will operate the line, assess knowledge transfer across those shifts rather than assuming that the first trained crew will teach everybody else consistently. The buyer should retain responsibility for the final authorization to operate, with the supplier’s technical handover evidence available to support that decision.
Keep Handover Current as the Plant Learns
After commissioning, review operating instructions when the accepted baseline, product mix, controls, or equipment arrangement changes. Preserve earlier revisions and explain why the new method was approved. Inform the affected operators and reassess the relevant tasks instead of expecting them to infer a change from a new setting on the screen. An operating window is useful only when the receiving team understands its conditions and knows which revision represents the current approved practice.
The strongest operator handover leaves a plant with more than a signed training sheet. It provides understandable routines, clear adjustment authority, traceable product transitions, and a practical communication method for exceptions. Those elements help the team reproduce successful operation while maintaining the distinction between ordinary production and specialist intervention. For the buyer, this is the durable value of the handover: stable start-stop and changeover behavior that belongs to the operating organization, rather than to one visiting technician’s memory.